language
 русский
 عربى
 Indonesia
Multistage High Pressure Booster Pump Wholesale


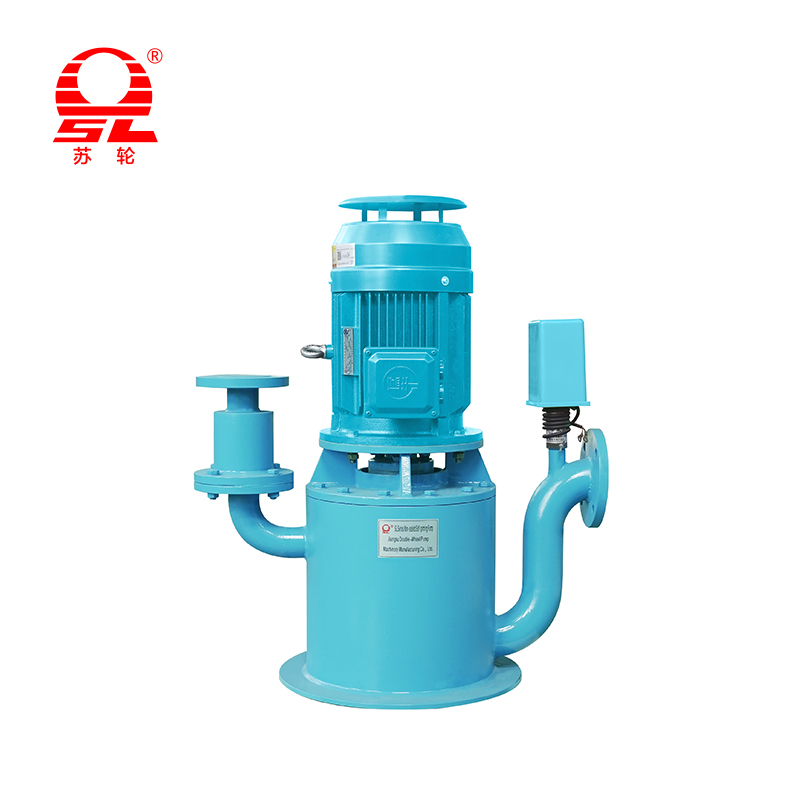

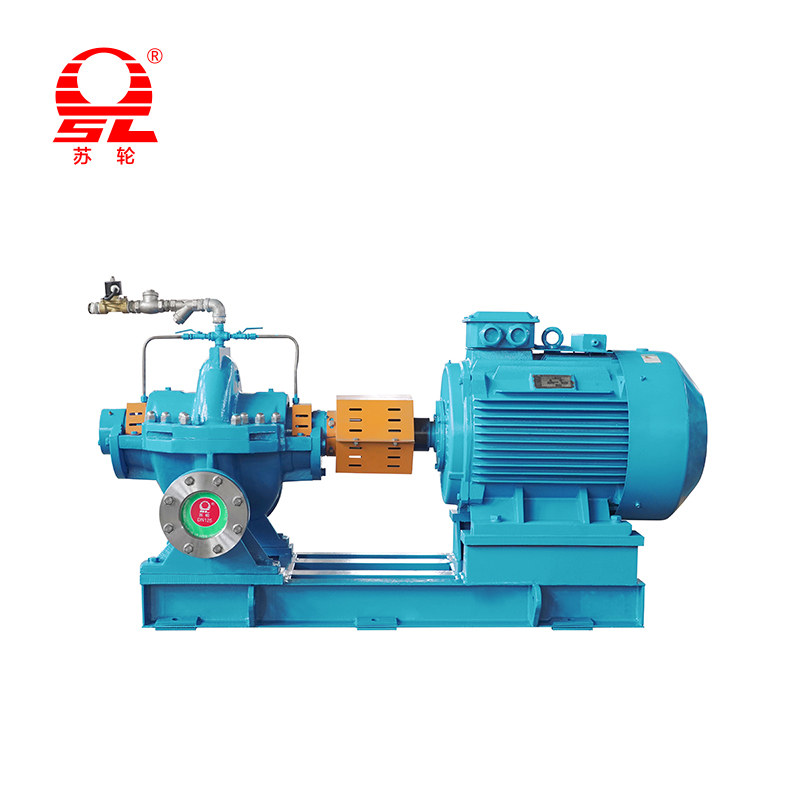
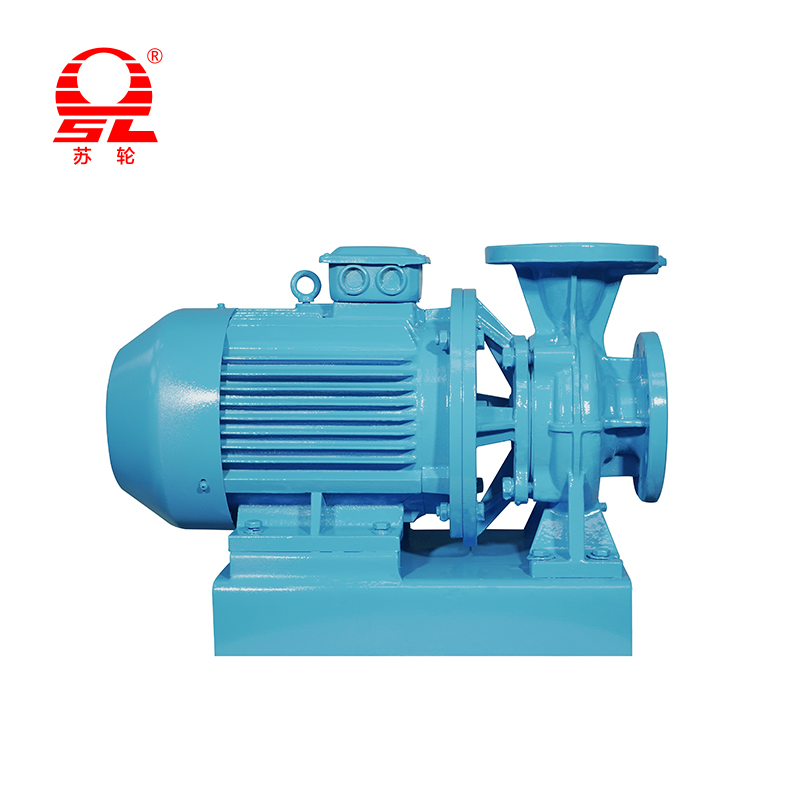


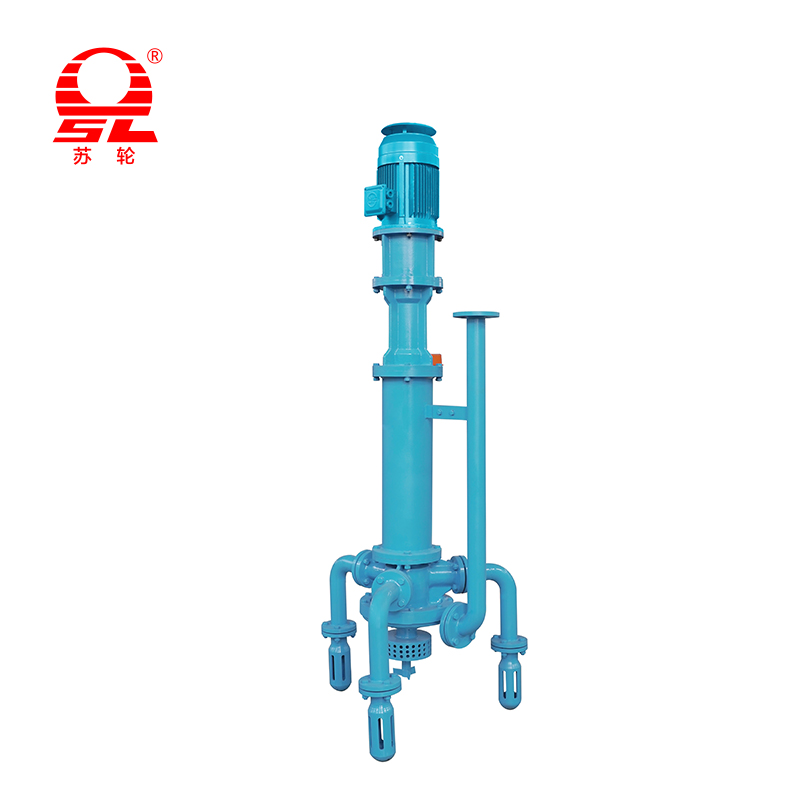

Up to 500m Head
High-Rise Rated
ISO 9001:2015
CE Certified
Fire Protection Approved
Multistage High Pressure Booster Pump
The MHB series stacks precision-matched impeller-diffuser stages inside a single casing to deliver high discharge pressure from a modest inlet supply. From high-rise domestic water boosting to fire protection systems and boiler feedwater duty, the same staged architecture scales simply by adding or removing stages — no redesign required.
Product Introduction
Precision-Staged Pressure for Demanding Water Systems
How the MHB Multistage High Pressure Booster Pump series converts modest inlet pressure into the high head that tall buildings, fire protection systems, and process boilers require.
The Multistage High Pressure Booster Pump solves a fundamentally different problem than a single-stage centrifugal pump: generating high discharge head from a relatively low-pressure water source. Rather than relying on one large impeller — which becomes mechanically impractical once head requirements exceed roughly 80–100 meters — the MHB series stacks multiple smaller impellers in series inside a single casing, with each stage adding its own increment of head to the water passing through it.
This staged architecture is why the same basic platform can serve a 40-storey high-rise domestic water booster set, a fire protection sprinkler system requiring sustained high pressure at the most remote hose cabinet, and a boiler feedwater application pushing against furnace pressure — applications with wildly different absolute pressure needs, met simply by varying the number of stages rather than redesigning the pump.
Each stage consists of a matched impeller and diffuser pair, precision-balanced as an assembly to keep radial and axial forces controlled as they accumulate across the stack. The cumulative axial thrust from multiple stages pushing in the same direction is countered by a balance disc or balance drum system, which redirects a small controlled leakage flow to neutralize thrust before it reaches the thrust bearing — a critical design detail that determines bearing life on any multistage pump.
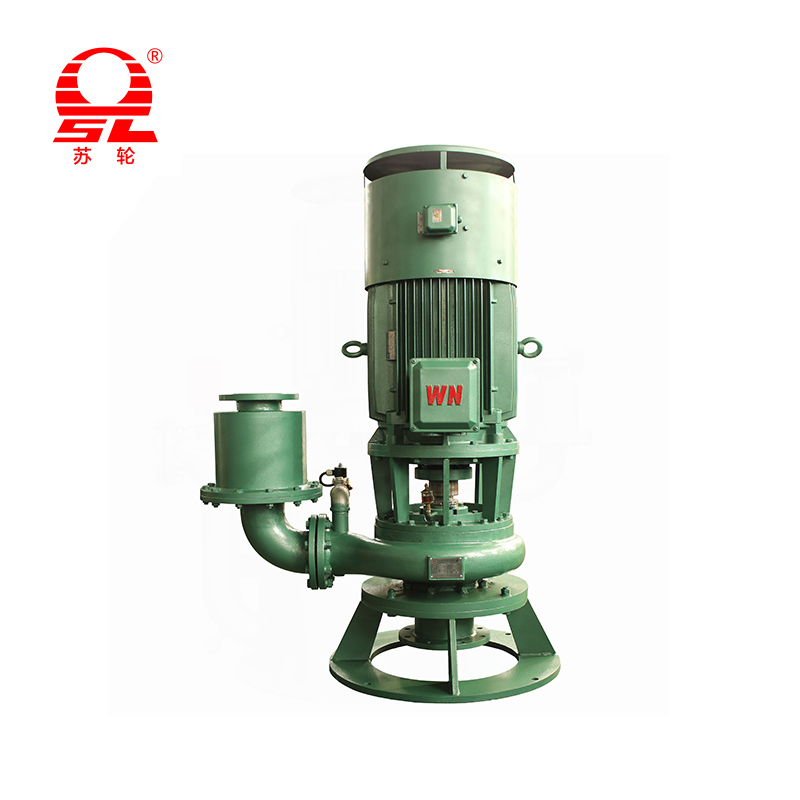
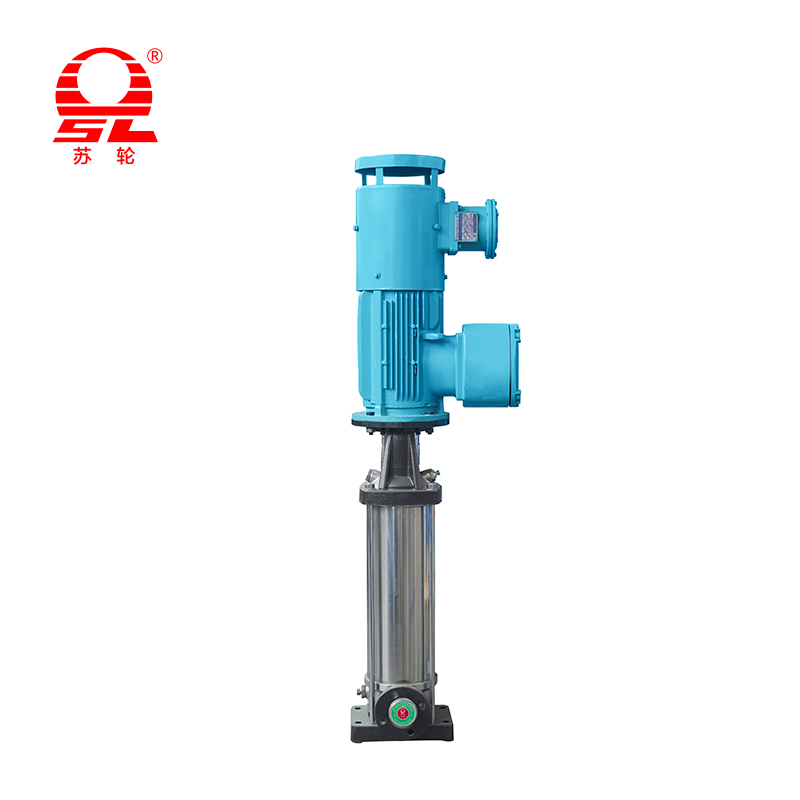
Vertical inline configurations minimize floor space in mechanical rooms and pump houses where every square meter matters, while horizontal split-case and ring-section configurations serve larger flow, lower-maintenance-access applications such as municipal water distribution boosting and industrial process feed. Both orientations share the same stage-and-diffuser hydraulic design, so performance data transfers directly between configurations.
Material selection responds to the duty: cast iron stages with bronze wear rings cover standard clean water boosting; stainless steel 304/316 stages serve potable water systems, food processing, and light chemical duty where corrosion resistance or hygiene standards require it; and duplex stainless variants extend service into more aggressive water chemistries such as brackish or lightly saline supply.
Every MHB unit is performance-curve tested at the factory across its full flow range to confirm head, efficiency, and NPSH required match the published curve before it ships — essential for multistage pumps, where even small manufacturing variances compound across multiple stages and can shift the delivered curve measurably from a single-stage design.
Vertical inline or horizontal split-case / ring-section configurations
Head range from 50 m to over 500 m via variable stage count
Balance disc / drum system controls accumulated axial thrust
Cast iron, SS304, SS316, and duplex stainless material options
Matched impeller-diffuser stage assemblies, factory balanced
Full-range factory performance curve testing before shipment
VFD-compatible for demand-based pressure control and energy saving
Serves high-rise water supply, fire protection, and boiler feed duty
Technical Data
Technical Specifications
Comprehensive performance parameters across the full product series — from compact units to large-scale industrial installations.
| Parameter | Specification |
|---|---|
Total Head Range | 50 m – 500 m (stage-dependent) |
Flow Rate Range | 5 m³/h – 650 m³/h |
Suction Requirement | Positive inlet pressure required (booster duty) |
Inlet / Outlet Diameter | DN 32 mm – DN 300 mm |
Motor Power Range | 2.2 kW – 500 kW |
Supply Voltage | 380 V / 6 kV (50 Hz / 60 Hz) |
Rated Speed | 1450 – 2950 rpm (VFD adjustable) |
Stage Material Options | Cast iron, SS304, SS316, duplex stainless |
Stage Count | 2 – 12 stages (custom configurations available) |
Max Working Pressure | Up to 4.0 MPa; higher on request |
Thrust Balancing | Balance disc or balance drum system |
Flange Standard | GB / DIN / ANSI / JIS |
Fire Protection Rating | UL/FM listed variants available on request |
Noise Level | ≤ 80 dB(A) at 1 m under rated load |
Certifications | ISO 9001:2015 · CE · UL/FM (optional) |
Why Choose It
Core Advantages
Six reasons engineers specify the MHB series for high-head applications where a single-stage pump reaches its practical limit.
Scalable Staged Architecture
Head requirement changes with stage count, not pump redesign — the same hydraulic platform covers a 50 m domestic booster set and a 500 m industrial feed application.
Compact Vertical Footprint
The vertical inline configuration stacks all stages within a small floor plan, freeing valuable mechanical room space in high-rise buildings and retrofit installations.
Controlled Axial Thrust
A dedicated balance disc or drum system neutralizes the accumulated axial thrust from multiple stages before it reaches the thrust bearing, directly extending bearing service life.
Fire Protection Ready
UL/FM listed variants meet the stringent, sustained-pressure demands of building fire sprinkler and standpipe systems, with performance verified at the most hydraulically remote point.
VFD-Compatible Energy Saving
Pairing the booster set with a variable frequency drive matches output to actual demand, cutting energy consumption significantly during the partial-load conditions that dominate most booster duty cycles.
Hygienic Material Options
SS304/SS316 stage construction meets potable water and food-processing hygiene requirements without sacrificing the head performance of the cast iron industrial range.
Use Cases
Primary Applications
Wherever a modest water supply must be converted into sustained high pressure across a demanding distribution system.
High-Rise Domestic Water Supply
Boosting municipal supply pressure to reach upper floors of high-rise residential and commercial buildings, with pressure-reducing zoning to protect lower-floor plumbing.
Fire Protection Systems
Maintaining sustained design pressure at the most remote sprinkler head or hose cabinet, sized to code-mandated flow and residual pressure requirements.
Boiler Feedwater
Overcoming furnace operating pressure to deliver feedwater into industrial and utility boilers at the head required for the specific boiler drum pressure.
Snowmaking Systems
Generating the high water pressure required to atomize water through snow gun nozzles at ski resorts and winter sports facilities.
Agricultural Irrigation
Pressurizing center-pivot and drip irrigation networks across large field areas where elevation change and pipeline friction loss both demand significant head.
Reverse Osmosis Pretreatment
Boosting feedwater pressure ahead of RO membrane trains in industrial water treatment, working alongside dedicated high-pressure RO feed pumps.
Head-to-Head
Performance Comparison
How the MHB multistage design compares with a single-stage centrifugal pump and a basic unbalanced multistage design.
| Feature / Criteria | This Series | Single-Stage Centrifugal Pump | Basic Unbalanced Multistage Pump |
|---|---|---|---|
| Achievable Head | Up to 500 m via staging | Limited to ~80–100 m practically | High, comparable |
| Footprint for High Head | Compact vertical inline option | Requires oversized impeller/casing | Similar footprint |
| Axial Thrust Management | Balance disc / drum system | Simple — single stage, low thrust | Often inadequate at high stage counts |
| Bearing Life at High Head | Extended via thrust balancing | Good — low thrust by design | Reduced — unmanaged thrust |
| Fire Protection Listing | UL/FM variants available | Rarely applicable at required head | Not typically listed |
| VFD Energy Optimization | Fully compatible | Compatible | Compatible |
| Factory Curve Verification | Full-range tested every unit | Standard practice | Less rigorous, stage variance risk |
Expert Tips
Usage Tips and Best Practices
Recommendations for getting reliable, efficient service from a multistage high pressure booster set.
1
Confirm Adequate Inlet Pressure
This is a booster pump, not a self-priming suction lift pump — verify your incoming supply pressure meets the minimum inlet requirement across the full expected demand range, including peak-hour low-pressure periods.
2
Size the VFD Control Band Correctly
Set the VFD's minimum and maximum frequency limits to keep the pump operating within its stable curve region; running too far below minimum speed on a multistage pump can create internal recirculation and premature wear.
3
Stage Redundancy for Critical Systems
For fire protection and other life-safety applications, install duty/standby booster sets with automatic changeover, since a multistage pump's high head performance is only as reliable as its single point of failure.
4
Monitor Balance System Leakage Flow
The balance disc or drum system relies on a small controlled leakage flow to function; periodically verify this flow path is not blocked by scale or debris, particularly in hard-water supply areas.
5
Avoid Prolonged Low-Flow Operation
Running significantly below minimum continuous stable flow generates internal recirculation and heat buildup across multiple stages; use a minimum-flow bypass line on systems with highly variable demand.
6
Verify Pressure Zoning on Tall Buildings
Install pressure-reducing valves at appropriate floor breaks so lower floors are not subjected to the full discharge pressure intended for the building's uppermost point.
FAQ
Frequently Asked Questions
Common technical questions from mechanical engineers and building services contractors specifying a booster pump set.
How many stages do I need for my head requirement?
Stage count is determined by your required total head divided by the head developed per stage at your design flow rate. Send us your required head and flow, and our engineering team will confirm the correct stage configuration and motor sizing.
Does this pump need positive inlet pressure to work?
Yes — the MHB series is a booster pump, designed to take in water at an existing positive pressure and raise it further. It is not a self-priming pump and should not be installed to draw from a tank below atmospheric pressure without a dedicated transfer/priming pump ahead of it.
What is a balance disc and why does it matter?
As water passes through multiple stages in the same direction, the cumulative force pushes the entire rotating assembly axially toward one end. The balance disc uses a controlled leakage flow to generate an opposing force, protecting the thrust bearing from a load it was never sized to carry directly.
Is this pump suitable for fire protection systems?
Yes, UL/FM listed variants are available specifically for fire sprinkler and standpipe applications, tested and certified to deliver the required flow and residual pressure at the hydraulically most remote point in the protected system.
Can I use a VFD to save energy on a multistage booster set?
Yes, VFD control is a standard and recommended approach for booster applications with variable demand — it can reduce energy consumption substantially during off-peak periods compared to constant-speed operation with a pressure-relief bypass.
What material should I choose for potable water applications?
SS304 or SS316 stage construction is recommended for potable water and food-grade applications, meeting hygiene requirements that cast iron construction, appropriate for industrial and fire protection duty, does not.
How is thrust bearing life affected by stage count?
Higher stage counts generate more cumulative axial thrust, which is why the balance disc/drum system is sized specifically to the stage count of each configuration — this is engineered into the design rather than left to a generic thrust bearing selection.
What documentation ships with the pump?
Each unit ships with a full-range factory performance curve test report, hydrostatic test certificate, material test certificates, and a CE Declaration of Conformity; UL/FM listed units include the applicable listing documentation.
Company
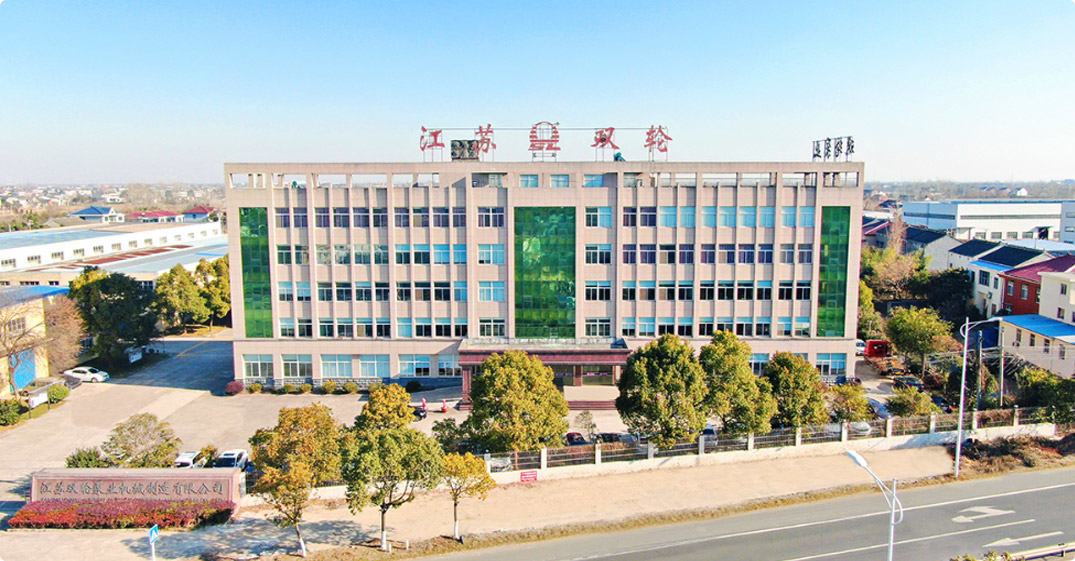
Jiangsu Double-wheel Pump Machinery Manufacting Co.,Ltd.
Jiangsu Double Wheel Pump Machinery Manufacturing Co., Ltd. is China Multistage High Pressure Booster Pump Manufacturers and Wholesale Multistage High Pressure Booster Pump Factory. The company is located in the scenic Yangtze River bank, Jiangyin Bridge, Beijing-Shanghai Expressway, Shanghai-Nanjing Expressway, Ningtong Expressway, Ningjingyan expressway running through the north and south, the traffic is very convenient, the geographical position is esteemed good. It is a production base specializing in non-sealed self-priming pumps, rain pumps, long-axis liquid pumps, chemical centrifugal pumps, positive displacement pumps and environmental protection equipment and mechanical equipment. The company has two production bases, covering an area of nearly 60,000 square meters, of which the eastern base covers an area of 33,000 square meters, the western base covers an area of 27,000 square meters, six modern production workshops, two installation workshops, a professional test workshop, a variety of mechanical processing equipment more than 160 sets, including a pump comprehensive performance test platform, Can test diameter 32-1200mm, motor power 1.1-1200KW, voltage 380V-10KV of various types of pumps, scientific research, development, manufacturing, processing, promotion, application of its own system. In the past two years, the company has closely followed the national industrial policy, made a big deal about environmental protection, and undertaken a large number of sewage treatment projects, which is unique in the environmental protection industry.
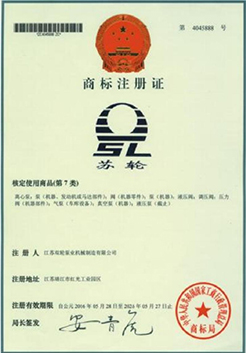
Certificate Of Honor


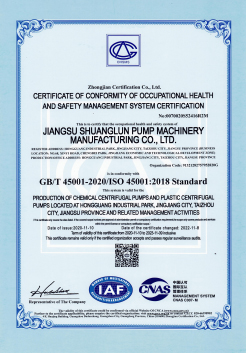
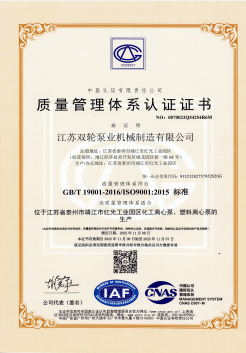
-
0

Be established in
-
0+

Professional personnel
-
0 million

Registered capital
-
0 ㎡

Plant area
After-Sales Service
Maintenance and Technical Support
Comprehensive support for booster set specification, from curve selection through commissioning of duty/standby systems.
Maintenance and Spare Parts
Stage-level serviceability minimizes downtime
- Complete Stage Cartridge Kits: Matched impeller-diffuser stage assemblies available as pre-balanced replacement cartridges, minimizing field rebalancing work during major overhauls.
- Balance Disc / Drum Wear Kits: Replacement thrust-balancing components sized to your specific stage count and configuration, restoring correct axial thrust management.
- Mechanical Seal and Bearing Kits: Genuine replacement seals and bearings machined to original tolerances for both vertical and horizontal configurations.
- 10-Year Spare Parts Commitment: Critical spare parts guaranteed available for a minimum of 10 years from purchase date, with priority stocking for fire protection and critical infrastructure customers.
Application Engineering Support
Curve selection backed by system hydraulics expertise
- System Curve and Stage Selection: Our engineers calculate your required head at design flow, including elevation change and pipeline friction loss, to confirm the correct stage count and motor sizing.
- Duty/Standby System Design: Guidance on redundant booster set configuration, automatic changeover logic, and alternation control for critical building water supply and fire protection systems.
- VFD and Control Panel Consultation: Recommendations on VFD sizing, pressure sensor placement, and control band settings for demand-based pressure control on variable-load systems.
- Fire Protection Code Compliance Support: Assistance interpreting local fire code flow and pressure requirements and matching them to the appropriate UL/FM listed configuration.


+86-0523- 84351 090 /+86-180 0142 8659

Welcome To
Jiangsu Double-Wheel Pump
Add 1: Hongguang Industrial Park, Jingjiang City, Jiangsu Province, China
Add 2: No.68, Xinyi Road, Industrial Park, Jingjiang City, Jiangsu Province, China
Contact
-
Tel:
+86-0523- 84351 090
+86-180 0142 8659 -
FAX:
+0523-8435 5588
- E-mail: